Remote Hydraulic Control for Coal Mines: Common Installation Challenges and Solutions
 A remote hydraulic control system rarely dies in the demo room. It dies at the 400-meter mark, where the cable tray twists, the hose bundle rubs, and coal dust finds every connector you swore was sealed. That is the uncomfortable truth about installing remote hydraulic controls in coal mines. The technology can be excellent on a test bench. Underground, it has to survive a place that seems designed to break it.
The good news is that most installation failures are not mysterious. They repeat. Crews hit the same walls in different mines: contamination, moisture, vibration, bad cable routing, hazardous-area approvals, pressure spikes, and the simple fact that production cannot stop for a two-week science project. Fix those early, and a remote hydraulic control system becomes what it was meant to be: safer, faster, and far less dependent on someone standing under unsupported roof.
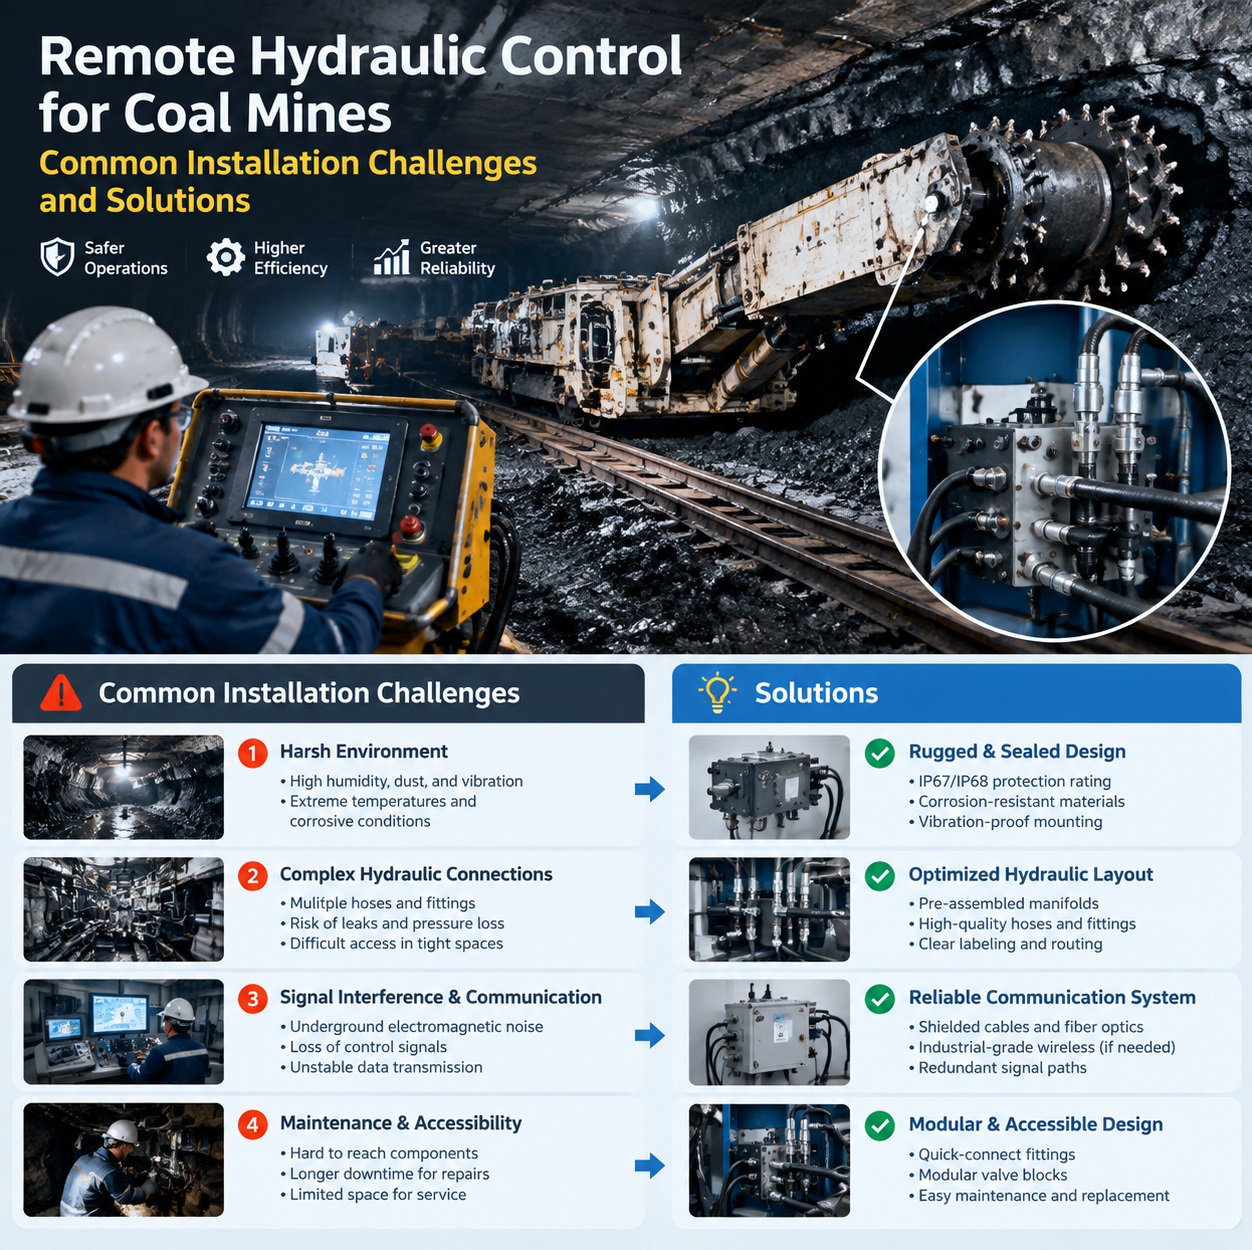
Dust and water do not care about your IP rating. Coal mines are wet, gritty, and abrasive. A control enclosure that passes a clean-room test can fail in a week when fine coal dust combines with acidic water and vibration. The solution is not one magic gasket. It is a system approach: IP68 or better enclosures, stainless steel or coated hardware, sealed connectors, proper cable glands, and mounting positions that keep boxes out of the spray zone. If the enclosure sits where roof water drips, move it. If a connector points upward, rotate it. Small installation decisions decide whether the system lasts months or years.
Hydraulic contamination is the silent killer. Remote hydraulic control adds more valves, manifolds, hoses, and quick-connects to a system that already lives in a dirty world. If the lines are not flushed and the fluid is not filtered to the correct cleanliness level, tiny particles will jam spools and erode seals. The fix is boring but non-negotiable: flush before connection, use high-pressure filtration during commissioning, cap every open port, and test fluid cleanliness before the first command is sent. A clean installation costs a few extra hours. A contaminated one costs downtime, replaced valves, and a maintenance team that stops trusting the remote system.
Long cable runs create their own kind of trouble. In underground coal mines, the distance from the operator station to the hydraulic valve bank can be hundreds of meters. That means voltage drop, signal noise, ground loops, and electromagnetic interference from motors, conveyors, and other equipment. A rugged cable is not enough. You need proper shielding, correct grounding, surge protection, and communication protocols that tolerate noise. Fiber optic segments can help on long runs. Redundant communication paths are even better. If the system loses signal for three seconds, the machine should fail safe, not freeze in a dangerous state.
Hazardous-area approvals can stall a project before installation begins. Coal mines require equipment that will not ignite methane or coal dust. Intrinsic safety, flameproof enclosures, and regional certifications are not paperwork decorations. They determine what you can install, where you can install it, and how you maintain it. The solution is to involve the supplier early and choose hardware that already carries the required approvals for your region. Do not assume a general industrial control box can be modified later. Retrofitting certification is expensive, slow, and sometimes impossible.
Pressure spikes are another common surprise. Hydraulic systems in coal mines do not always behave like gentle textbook circuits. Roof support movements, sudden valve closures, and thermal expansion can send pressure spikes through the lines. If the remote control manifold and hoses are not rated for those peaks, fittings weep, seals fail, and sensors drift. Use pressure relief, accumulators where appropriate, and hose assemblies with the correct burst rating. Route hoses away from moving machinery and sharp edges. A hose that rubs against a steel edge for one shift can become a leak by the next.
Then there is the human side. A remote hydraulic control system is only as good as the people who install, operate, and maintain it. If the interface is confusing, operators will bypass it. If the diagnostics are hidden, technicians will guess. If the training is a PDF and a handshake, mistakes will repeat. Good suppliers provide hands-on commissioning, clear schematics, labeled components, and training that matches the actual mine layout. They also design for maintenance access. A valve bank that requires removing a guard, crawling into a tight space, and disconnecting three hoses just to check a fuse will not get checked.
Commissioning is where all these challenges meet. The mine still needs production. The installation window is short. The environment is hostile. The best way to avoid chaos is to pre-assemble and factory-test as much as possible. Modular valve skids, pre-wired enclosures, labeled hose bundles, and plug-and-play connectors reduce underground labor. A phased commissioning plan lets you test communication, hydraulics, safety interlocks, and remote operation in stages. That way, when the system goes live, the crew is verifying a known design, not discovering surprises.
None of this is glamorous. It is the difference between a remote hydraulic control system that looks good in a brochure and one that keeps working after the first month of coal dust, water, vibration, and heavy use. The mines that get it right treat installation as part of the engineering, not as an afterthought. They choose hardware that fits the environment, demand proper filtration and sealing, plan cable and hose routes carefully, and partner with a supplier who understands that underground support does not end when the purchase order is signed.
If you are planning a new remote hydraulic control installation or retrofitting an existing coal mine, start with the challenges. Map the environment. Check the approvals. Flush the lines. Protect the cables. Train the crew. Then let the technology do its job. The payoff is not just a smoother install. It is fewer people exposed to dangerous areas, less unplanned downtime, and a hydraulic control system that earns trust shift after shift.
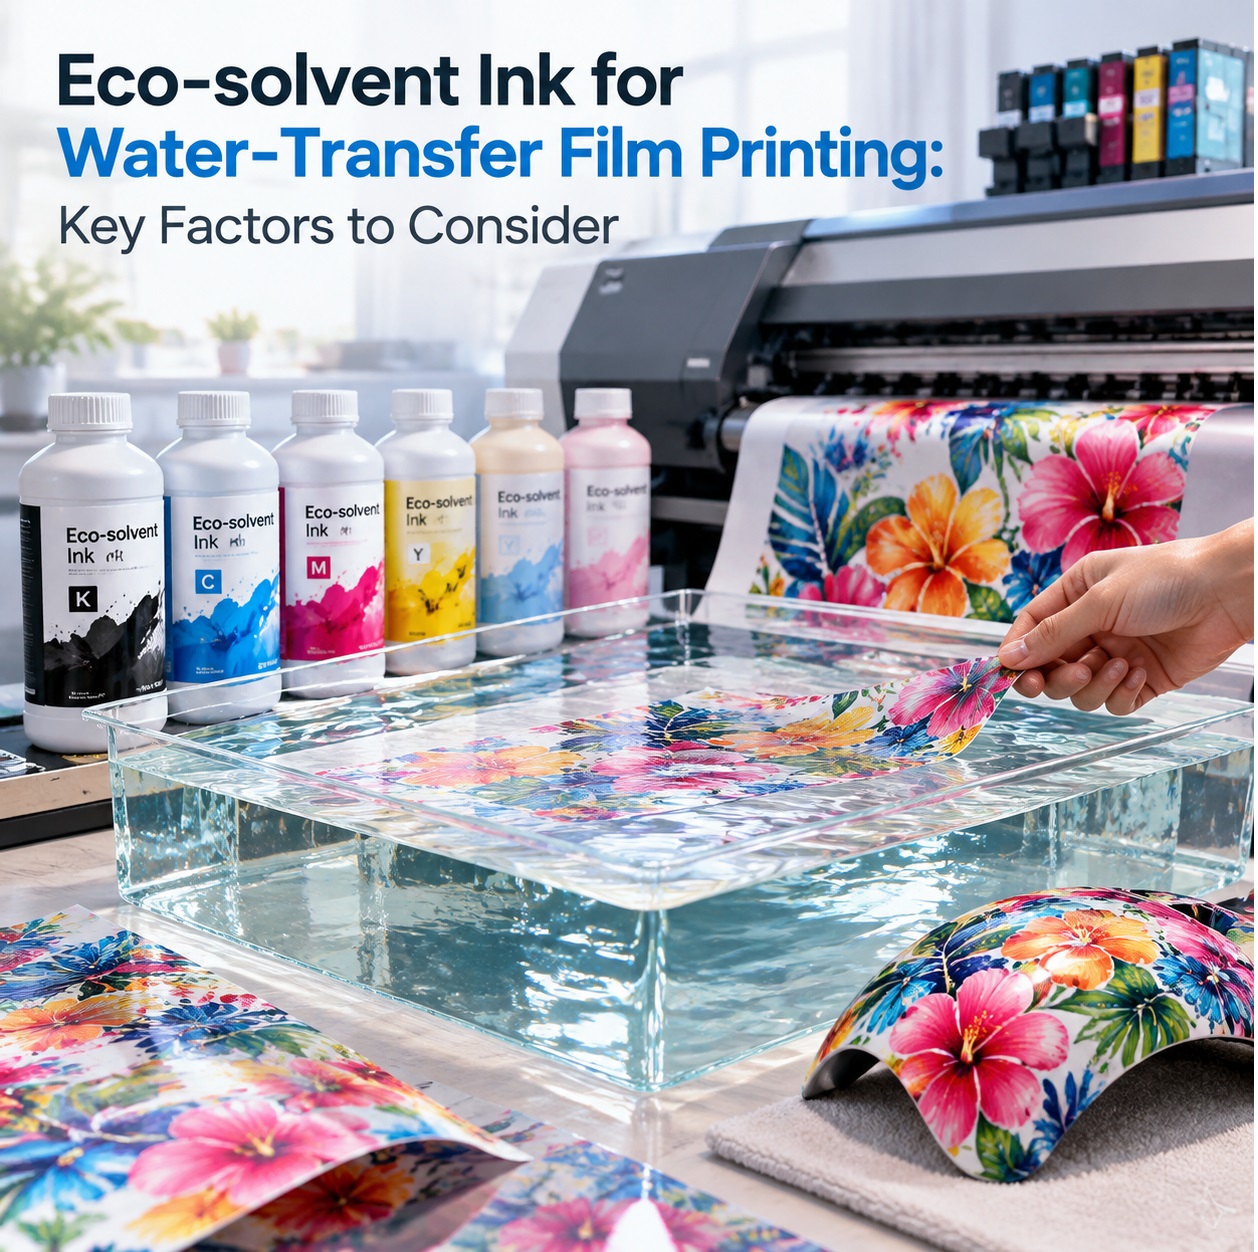 Most water-transfer film failures don’t announce themselves at the printer. They show up in the water bath, three seconds before the decal wrinkles, tears, or refuses to slide off its backing. By then the ink has been paid for, the film has been paid for, and the labor is gone.